Common problems encountered during plastic film blowing include: film being too sticky, poor film opening, poor film transparency, film wrinkling, water-like streaks on the film, uneven film thickness, film being too thick, film being too thin, poor heat sealing properties, poor longitudinal tensile strength, poor transverse tensile strength, unstable bubbles in the film, rough film surface, uneven surface, and odor. Below are the causes and solutions for these common problems.
Common problems encountered during plastic film blowing include: film being too sticky, poor film opening, poor film transparency, film wrinkling, water-like streaks on the film, uneven film thickness, film being too thick, film being too thin, poor heat sealing properties, poor longitudinal tensile strength, poor transverse tensile strength, unstable bubbles in the film, rough film surface, uneven surface, and odor. Below are the causes and solutions for these common problems.
1. Film too sticky, poor opening
Causes: ① Incorrect resin type; not using blow-molding grade LDPE resin granules, or insufficient or no end-group modifier; ② Excessive melt temperature, resulting in excessive flow; ③ Excessive inflation ratio, leading to poor film opening; ④ Insufficient cooling, causing the film to stick together under the pressure of the rollers; ⑤ Excessive pulling speed.
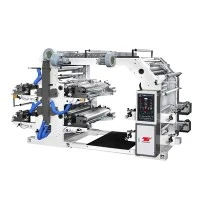
Plastic Film Blowing Machine
Solutions: ① Replace the resin or add a suitable amount of dispersant; ② Reduce the extrusion and resin temperatures; ③ Reduce the inflation ratio; ④ Increase airflow to improve cooling and speed up film cooling; ⑤ Reduce the pulling speed.
2. Poor film transparency
Possible causes: ① Insufficient extrusion temperature, resulting in poor resin melt flow and poor transparency of the film; ② Insufficient inflation ratio; ③ Inadequate cooling, affecting film transparency; ④ Excessive moisture content in the resin raw material; ⑤ Excessive pulling speed of the film blowing machine, resulting in insufficient cooling of the film.
Solutions: ① Increase the extrusion temperature to ensure uniform resin melt flow; ② Increase the inflation ratio; ③ Increase the airflow of the film blowing machine to improve cooling; ④ Dry the raw material; ⑤ Reduce the pulling speed.
3. Film wrinkling
Possible causes: ① Uneven film thickness; ② Insufficient cooling; ③ Excessive inflation ratio, causing unstable film bubble and resulting in wrinkling; ④ Excessive clamping angle of the film blowing machine, causing the film to be flattened and prone to wrinkling.
Solutions: ① Adjust the film thickness to ensure uniformity; ② Improve cooling to ensure complete cooling of the film; ③ Reduce the inflation ratio; ④ Reduce the clamping angle of the film blowing machine to ensure even stress on the film.